Carter CNC press brakes

Press brakes built for accurate bending.

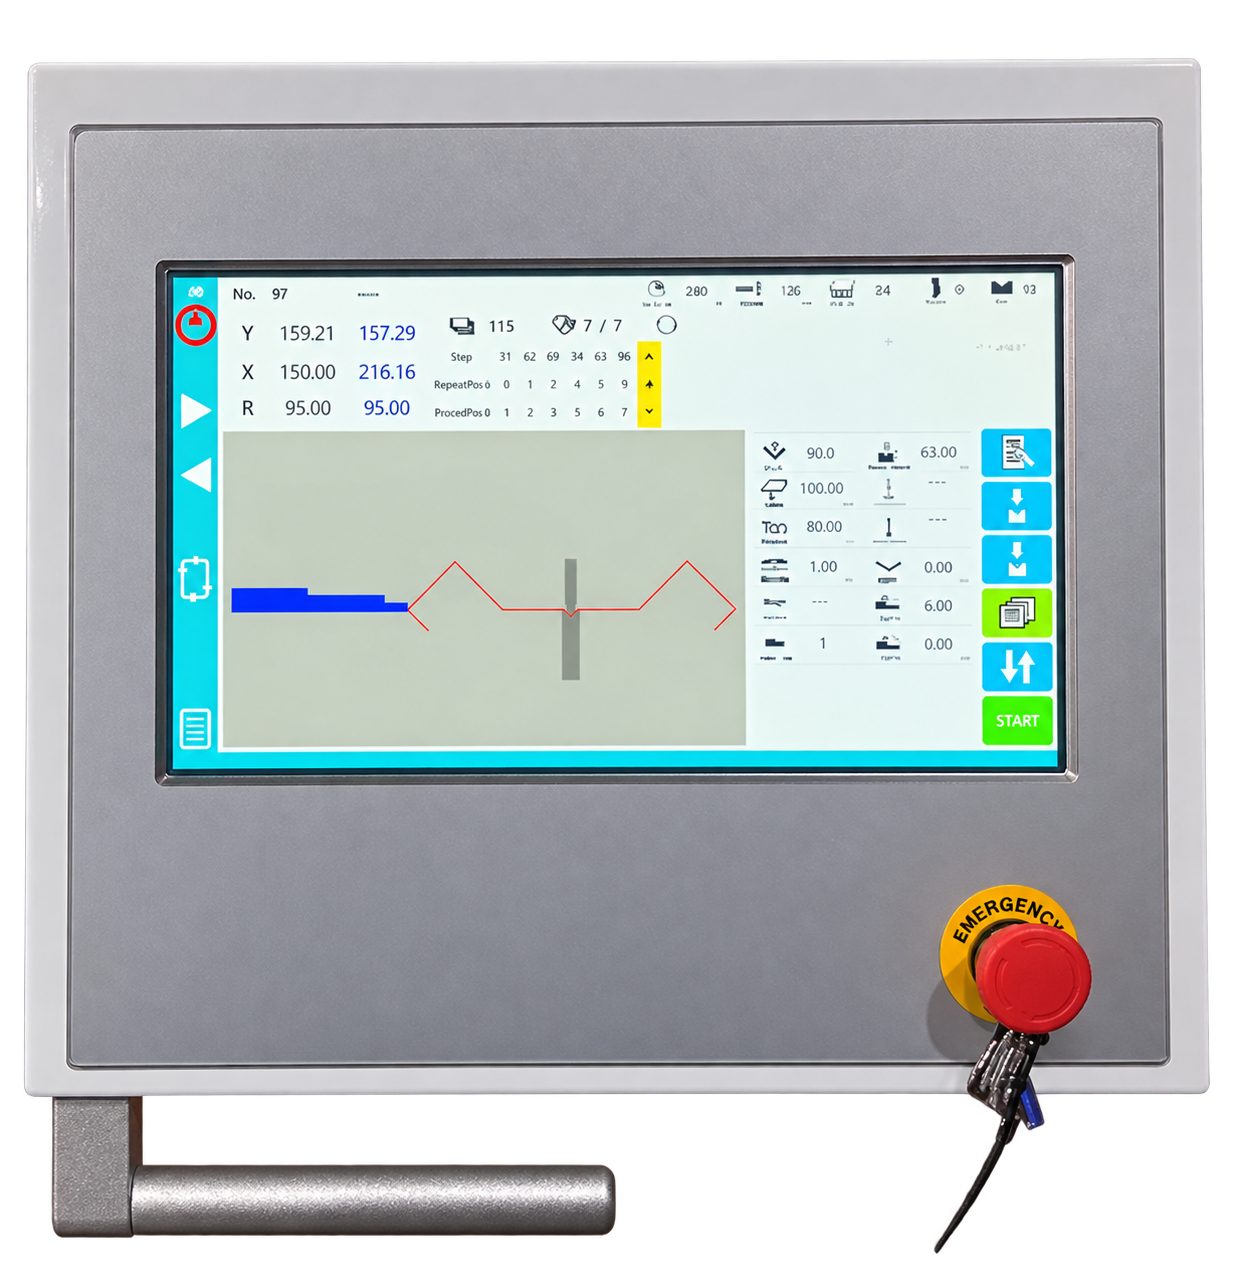
Choose a 5-axis CNC press brake to suit your bending length and tonnage. The range includes a graphical controller, safety equipment and standard Euram tooling.

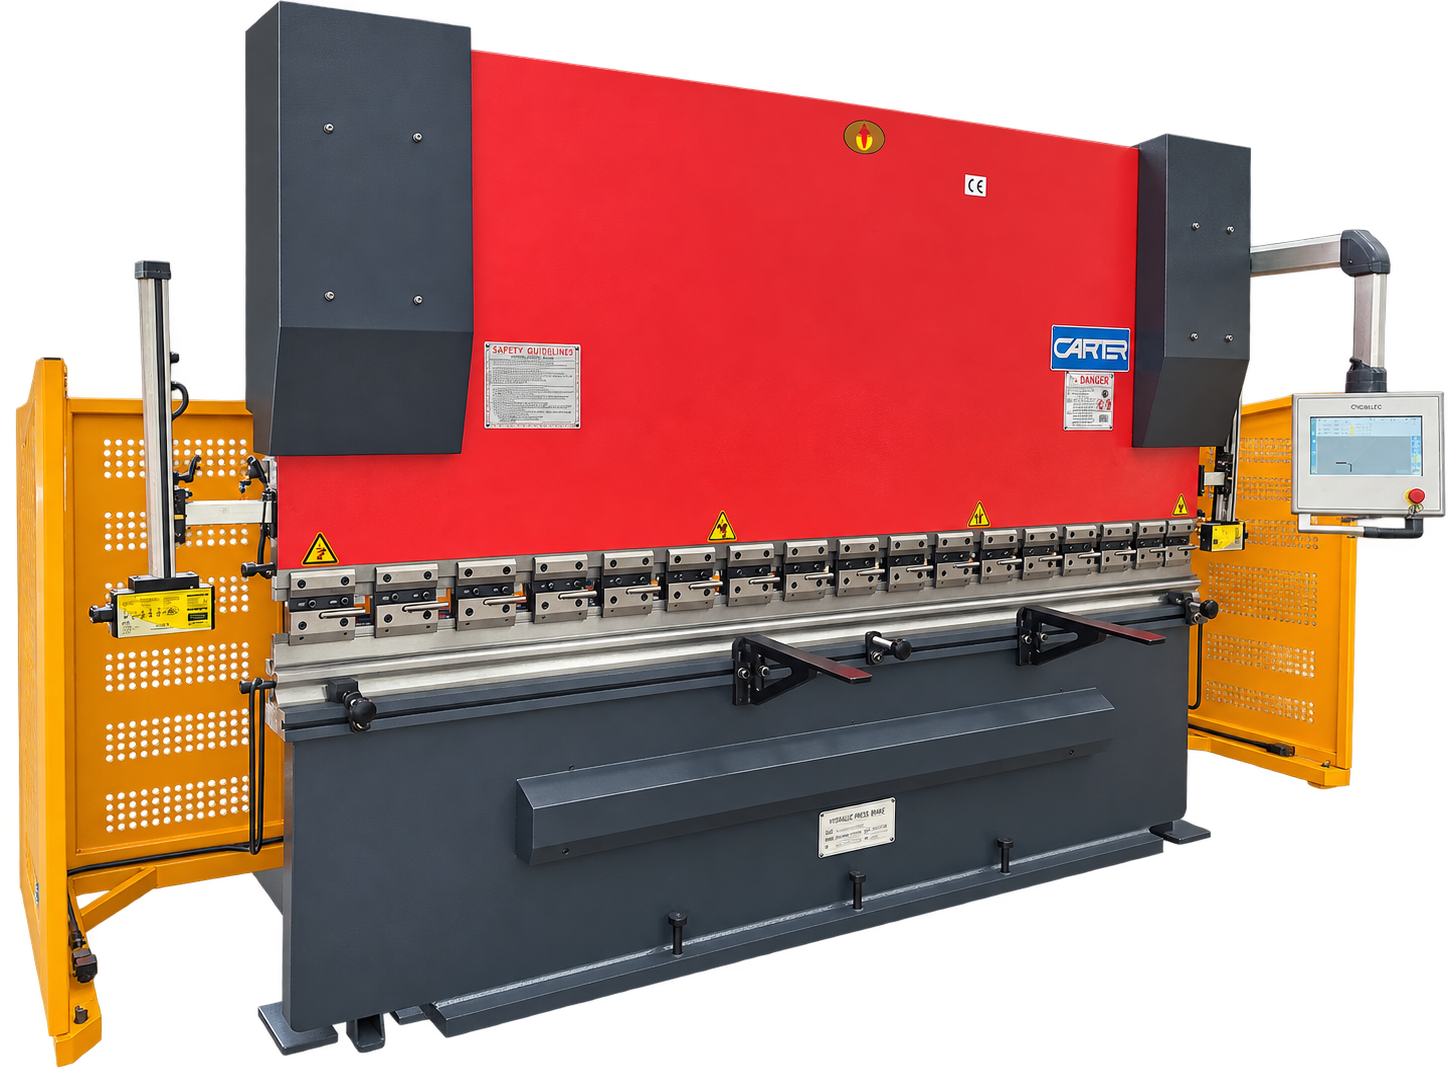
Featured machine: new 3400 × 125T CNC press brake · £30,883 + VAT and delivery

Carter red and charcoal five-axis press brake with yellow laser guards
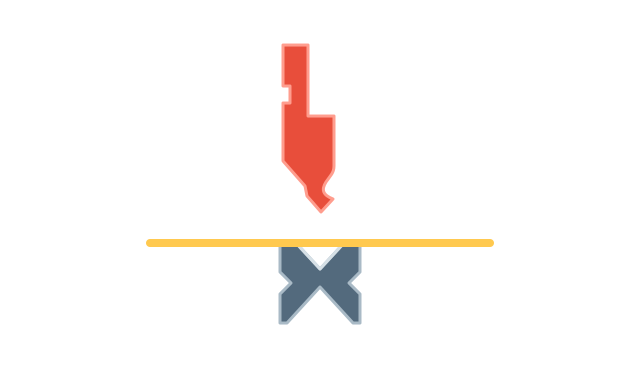
Air-bending example using a Euram 1010 punch with the 2009 four-V die; the punch moves down and the die stays fixed.
Example tools: Euram 1010 punch · 2009 four-V die
New Carter 5-axis CNC press brakes

Find the right press brake capacity

All prices below are + VAT and delivery. Ask us to confirm availability and the specification for your chosen size. Larger sizes available on request.

Standard equipment across the range
  • Model 1010 gooseneck top tooling and a multi-V bottom tool fitted as standard
  • Commissioning, basic training and 12 months parts and labour warranty

Enquire about this size

Download the Carter price brochure (PDF)

Tap a feature photograph to view it full size.

Carter machine details

Built for controlled, repeatable bending

Images show representative press-brake equipment. Your quotation confirms the specification for the capacity you choose.

Tap a photograph to view it full size.

Five-axis CNC control

What each control changes

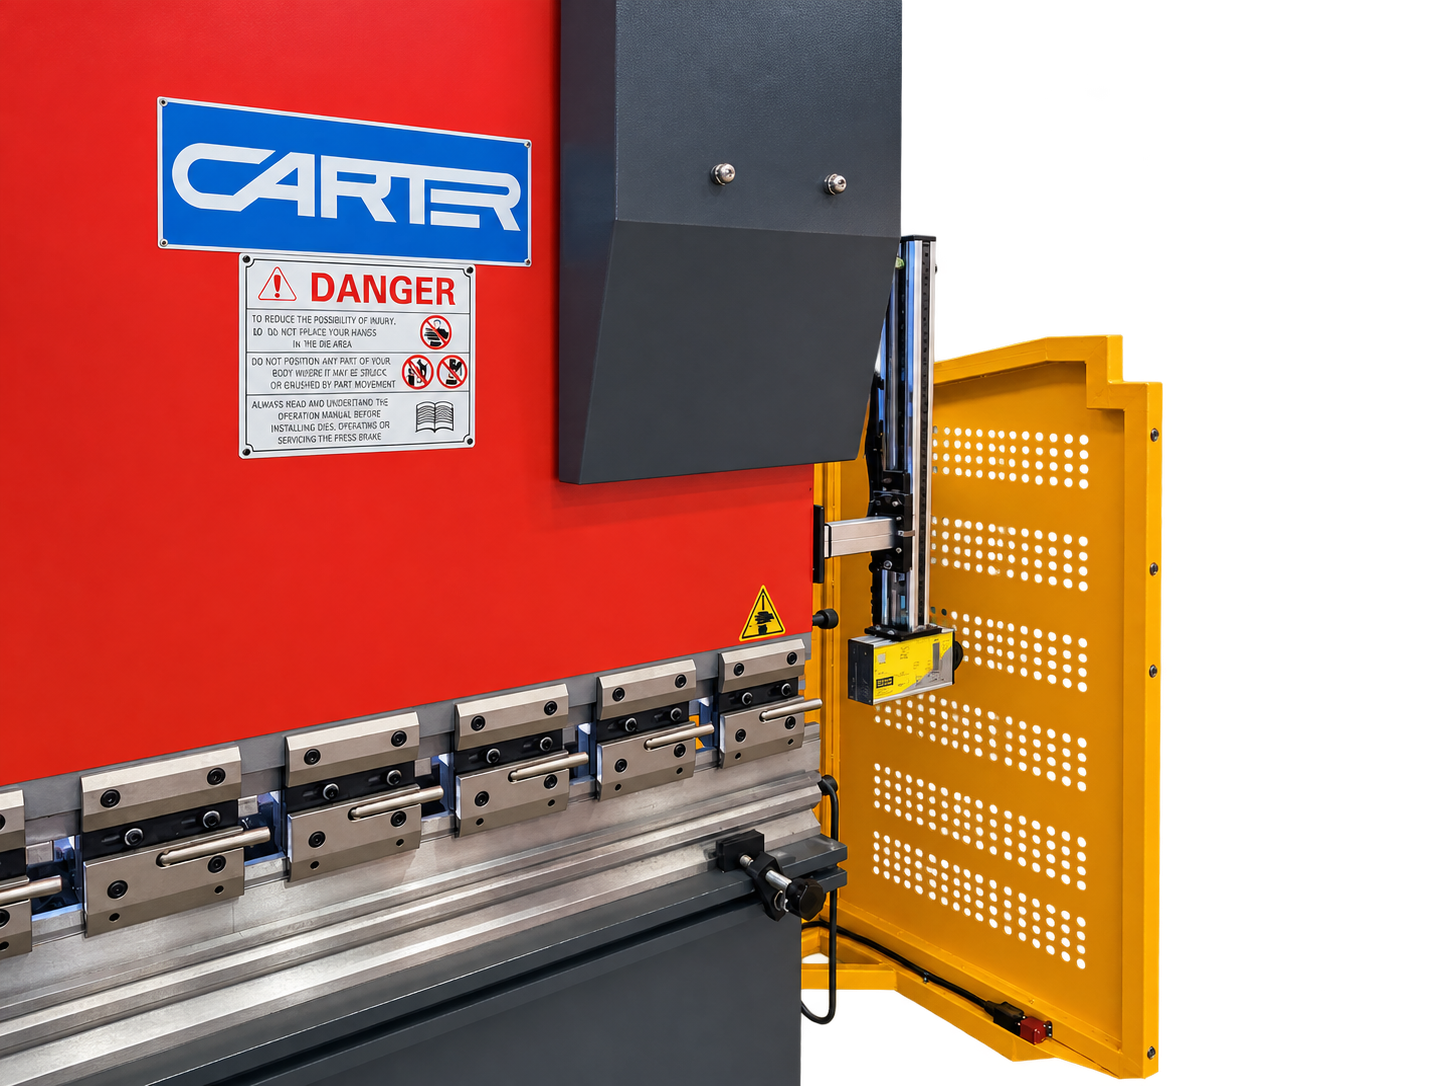
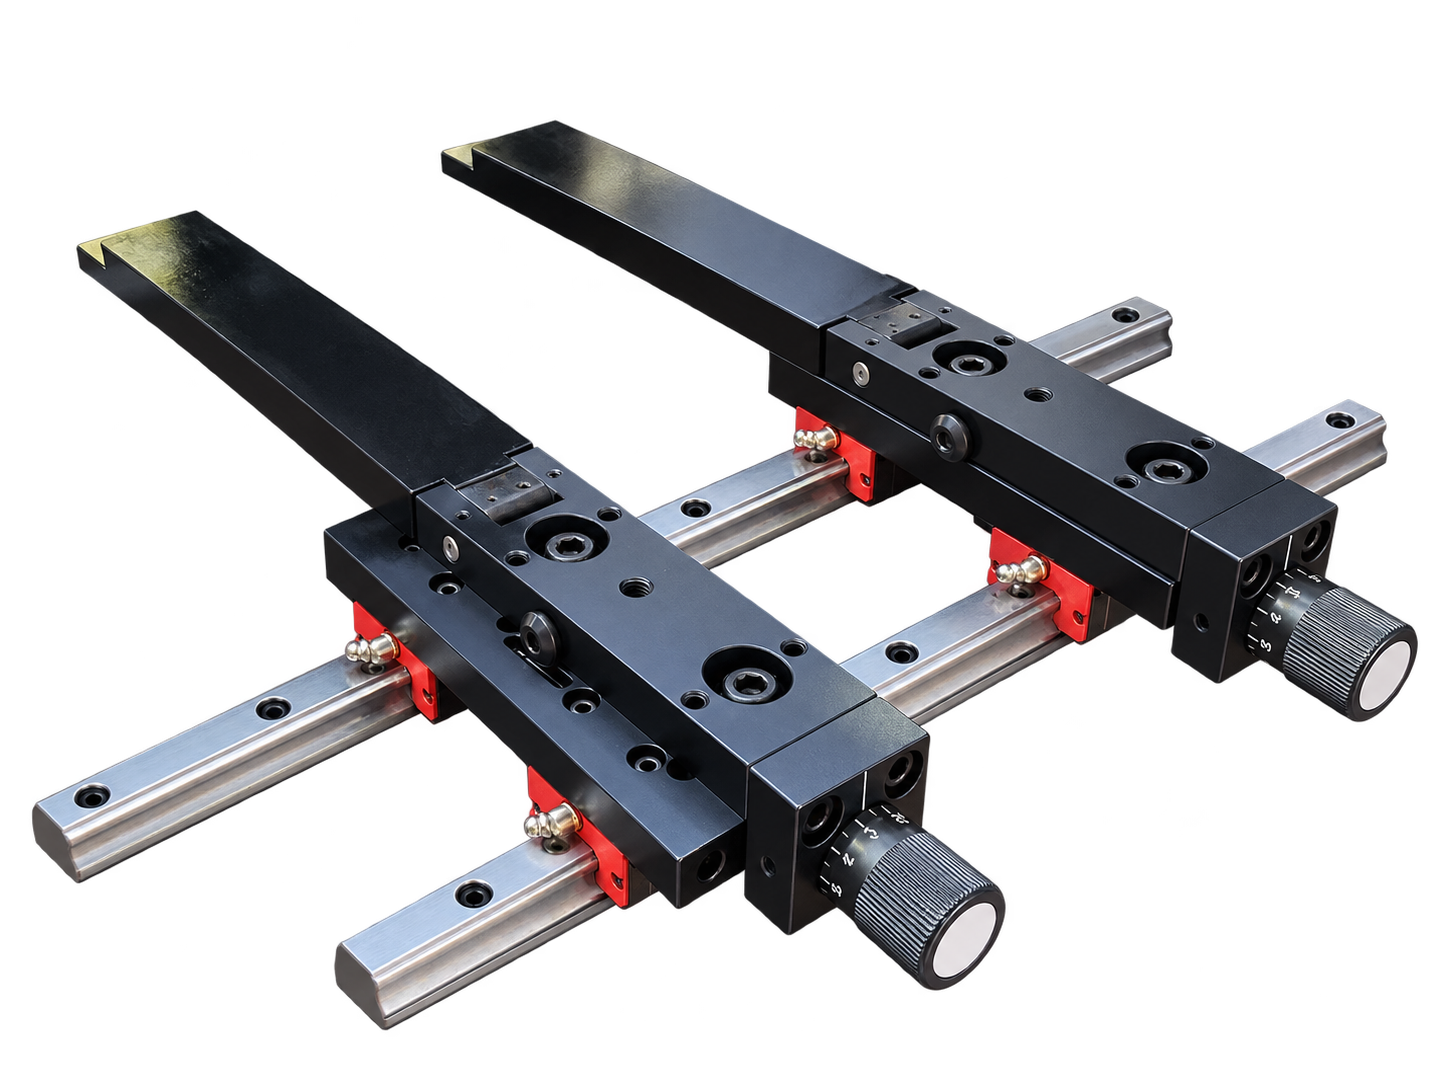
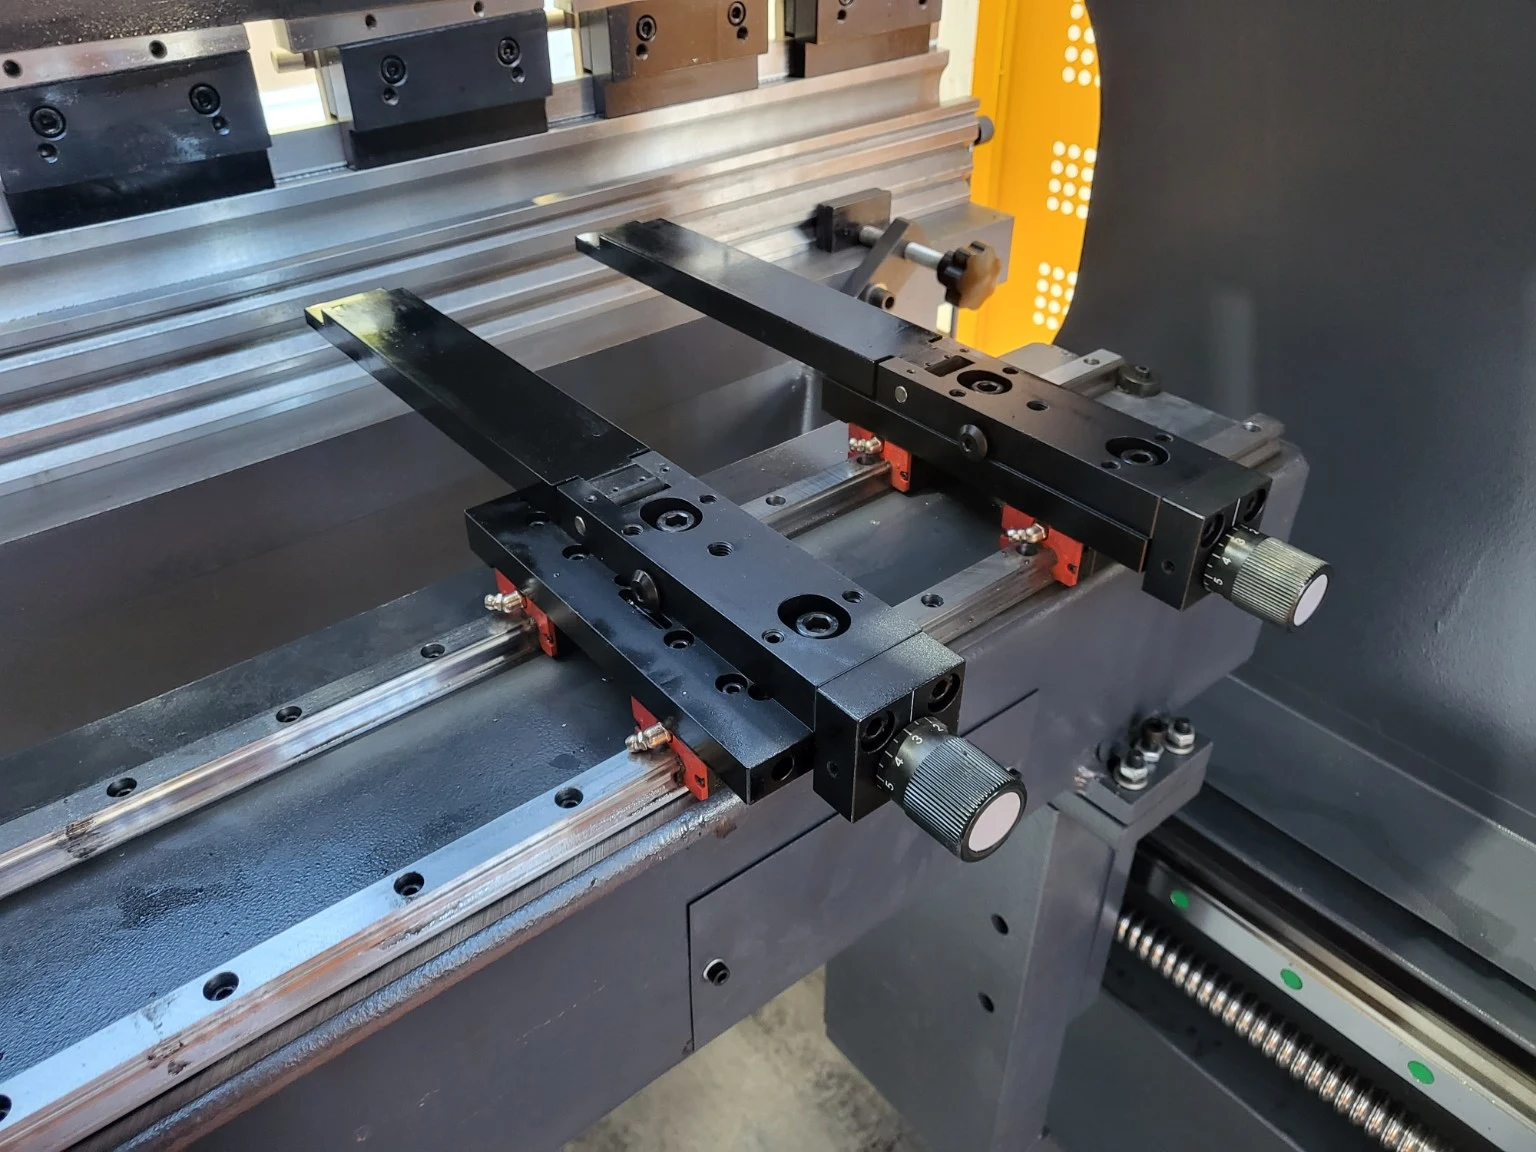
This Carter press brake uses Y, X, R, P and ADS. The labels below describe the actual machine controls; the photograph shows its backgauge fingers in place.

Y · Upper beamMoves the ram and punch up or down to form the bend.
X · Backgauge depthMoves both stop fingers towards or away from the tooling.
R · Backgauge heightRaises or lowers both stop fingers.
P · Bending pressureThe controller sets the required bending force for the job.
ADS · Anti-deflection systemThe controller calculates correction automatically; powered mechanical wedges adjust the bed support.
Actual Carter press-brake backgauge, showing the two adjustable fingers mounted behind the tooling
Actual press-brake backgaugeX moves the fingers in or out; R changes their height.

Z1/Z2 · Manual finger spacing
Each finger slides across the machine width by hand. Z1 and Z2 are not powered CNC axes.

ADS · anti-deflection system

Powered mechanical crowning

As bending force rises, the beam and bed can deflect along their length. The ADS controller calculates the required correction automatically, then powered mechanical wedges adjust bed support to help maintain a consistent bend angle from end to end.

Illustration is schematic; required crown depends on the machine, material, thickness and bend length.

Powered mechanical press-brake crowningA press-brake ram applies downward force along the bending line. Powered wedges adjust the lower bed support upward at the centre to compensate for deflection.RAM · BENDING FORCEDIE / WORK SUPPORTPowered wedges adjust support along the bed
Select compatible tools

Press brake tooling for your setup

Browse the Euram punches and dies catalogue or use the bending guide to estimate force and preview a bend setup.

Talk to Carter

Have a machine question?

Call for sales, spares, service or a quotation.

Flexible Payment Options

Bank transfer and Bitcoin payments accepted. Finance options are also available, subject to approval.

0800 644 4045sales@cartermachinery.co.ukWhatsApp 07508 035871Visit our eBay shopScott House, Clarke Street, Poulton-le-Fylde, Lancashire FY6 8JW