24-month parts-and-labour warranty
New Carter press brakes include commissioning and basic training.
3T × 200 mm to 60T × 2000 mm
All-electric bending from compact precision components to larger sheet metal work. Choose the bending length and force for your parts.
From £10,118.49 + VAT (£12,142.19 including VAT) and delivery
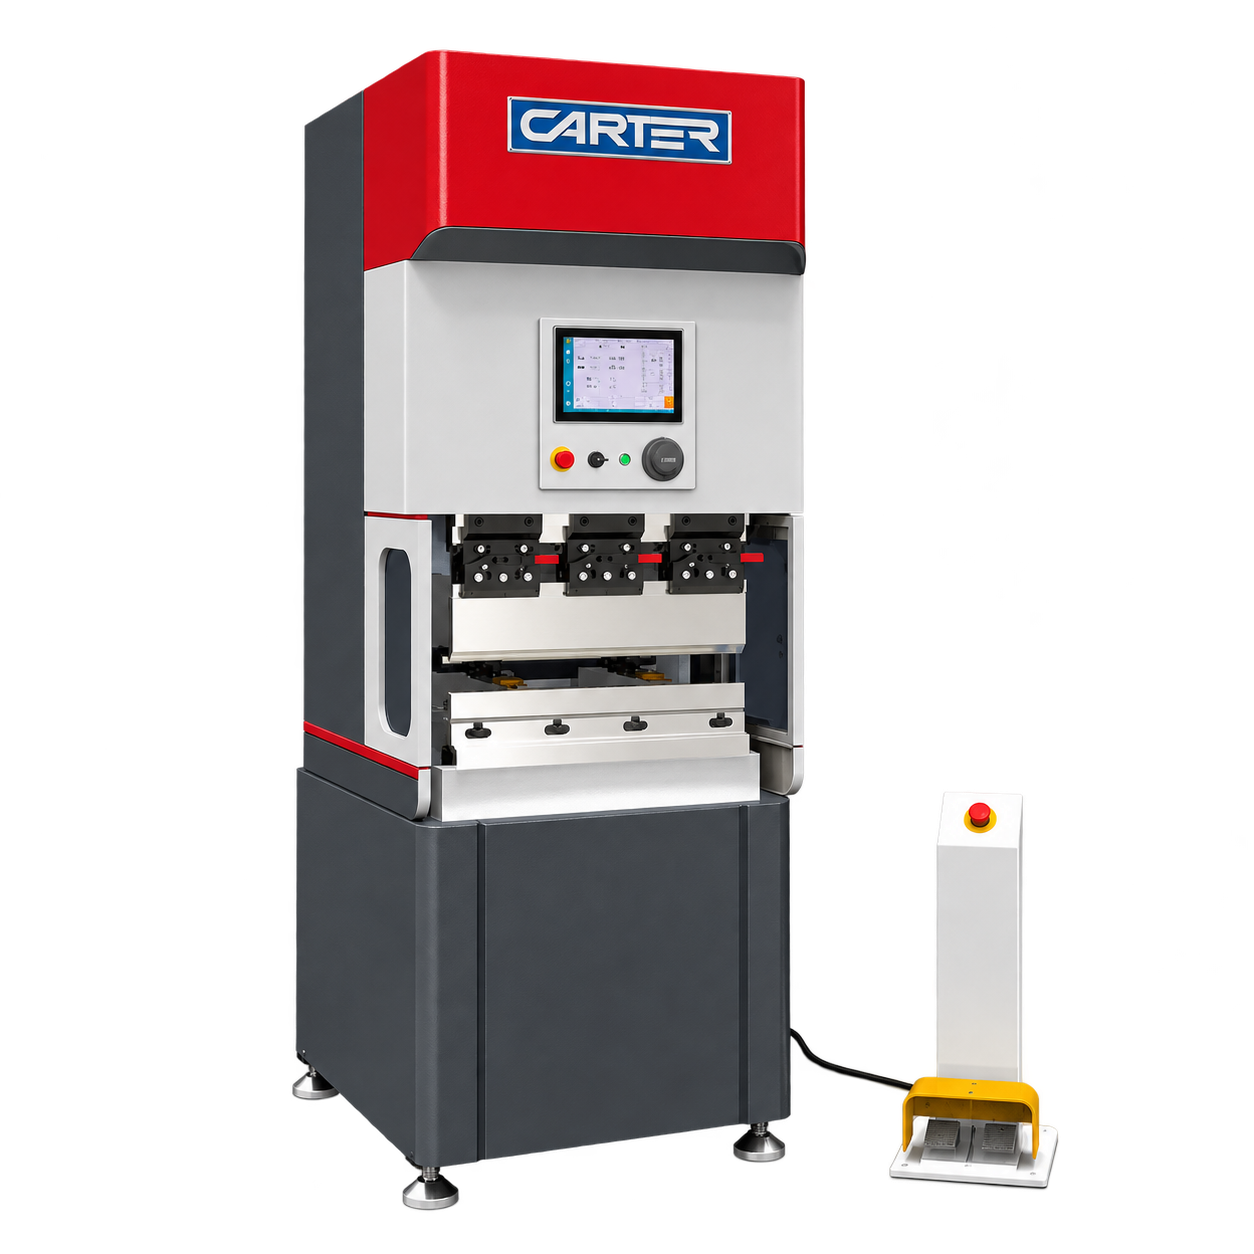 12T × 600 mm model shown. Larger machines have different frames and equipment.
Your machine. Your specification.
Choose a model to view its price and specification.
Powered crowning on 2,000 mm models only.
Guide prices are subject to confirmation of the selected machine and equipment.
Final tooling, guarding, electrical supply and machine configuration are confirmed in your quotation.
ENQUIRE ABOUT THIS MACHINE →| Model | Carter 12T × 600 mm |
|---|---|
| Bending force | 120 kN / 12T |
| Bending length | 600 mm |
| Drive configuration | Single servo |
| Distance between columns | 520 mm |
| Throat depth | 200 mm |
| Controlled axes | 3 (Y, X, R) |
| Main servo motor | 7.5 kW |
|---|---|
| Rapid approach speed | 200 mm/s |
| Bending speed | 15 mm/s |
| Backgauge travel | 200 mm |
| Controller display | 10.1″ |
| Machine weight | 1050 kg |
| Dimensions (L × W × H) | 770 × 1050 × 2150 mm |
Single-servo compact models use Y, X and R. Dual-servo models use independent Y1 and Y2 ram control, plus X backgauge depth and R backgauge height.
Sets the ram depth for the required bend angle.
Moves the backgauge forwards and backwards to set the flange length.
Raises and lowers the backgauge for different bend stages.
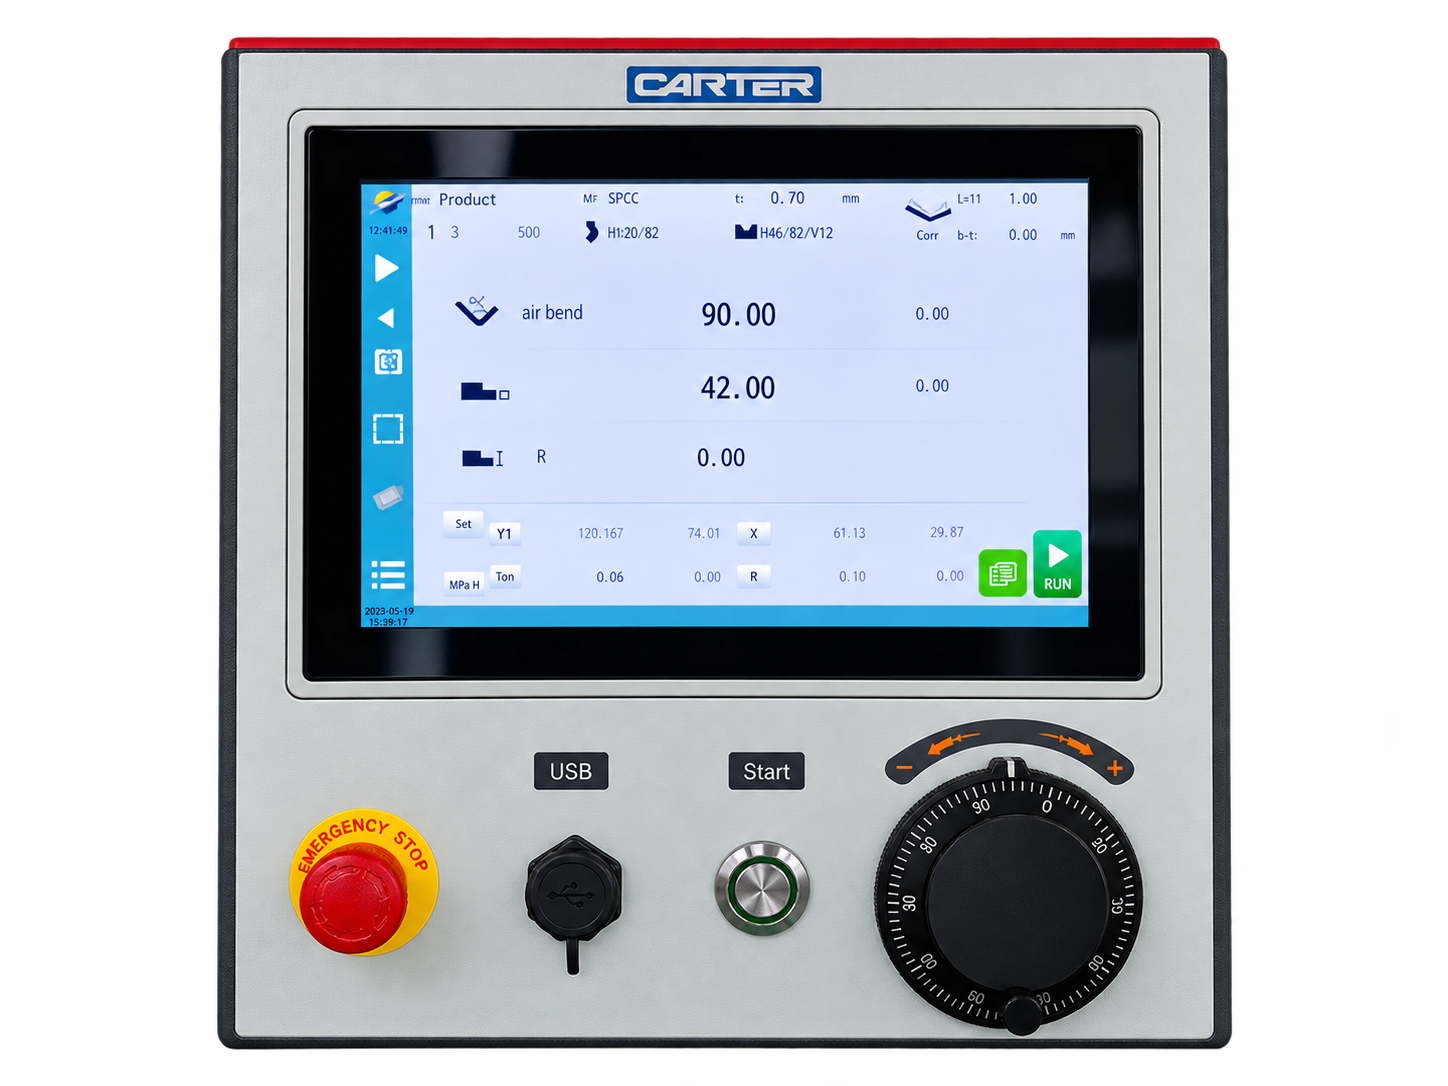
A closer look
12T × 600 mm model shown. Larger machines have different frames and equipment.
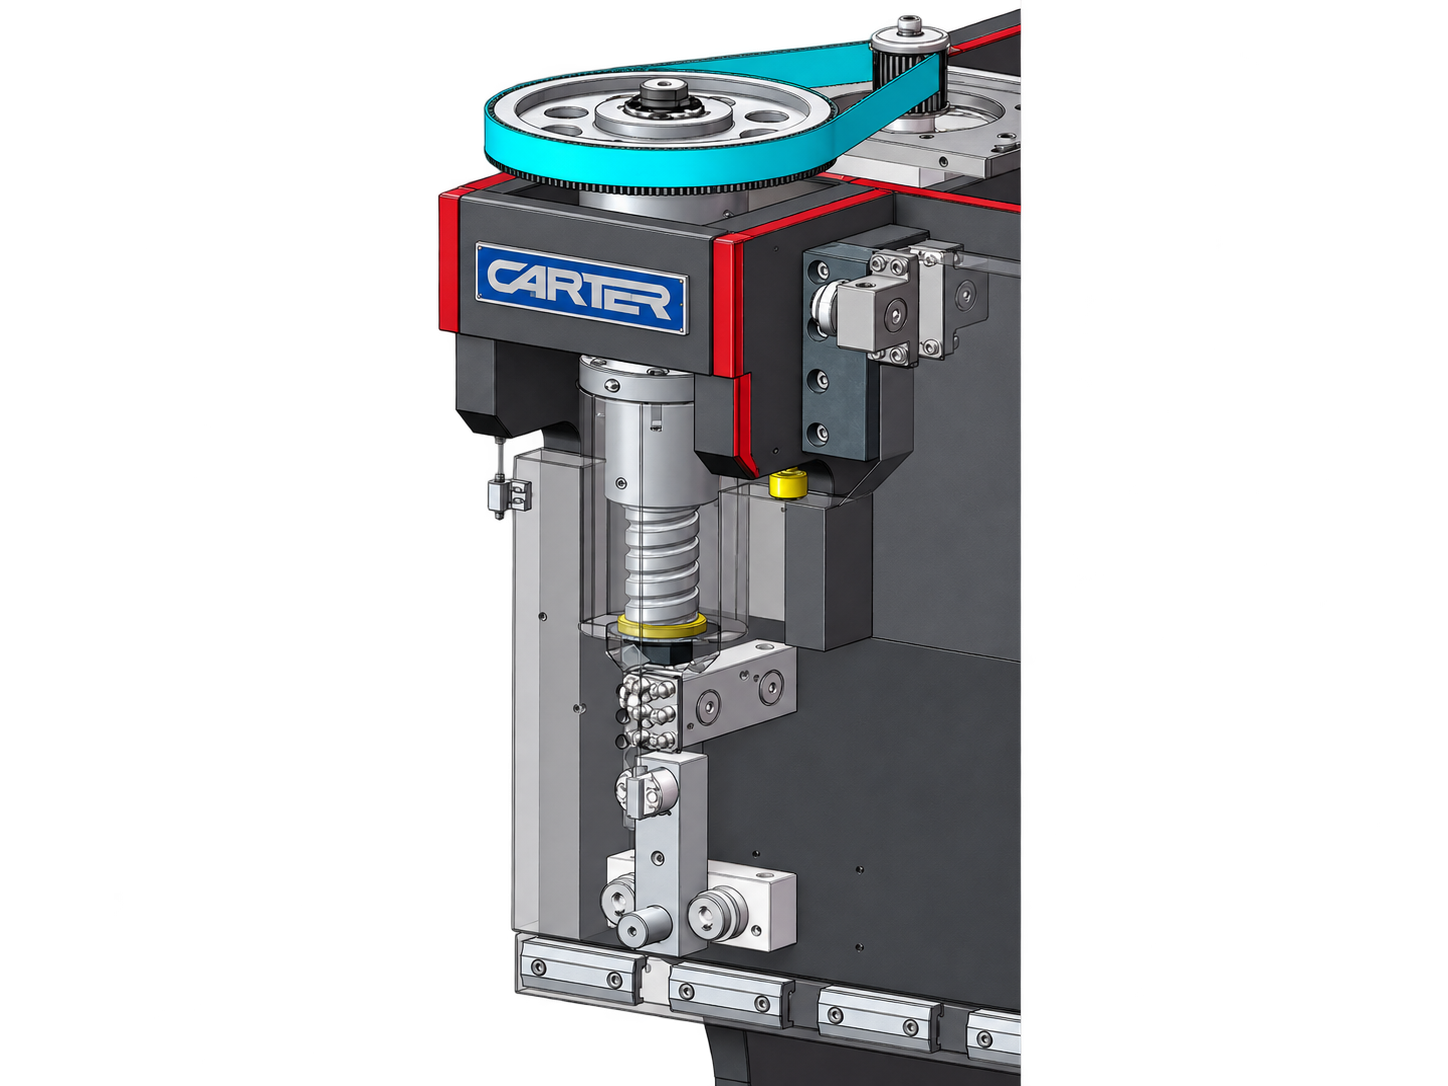
Direct servo drive through a precision ball screw delivers controlled ram movement and repeatable positioning, without a hydraulic pump or oil tank.
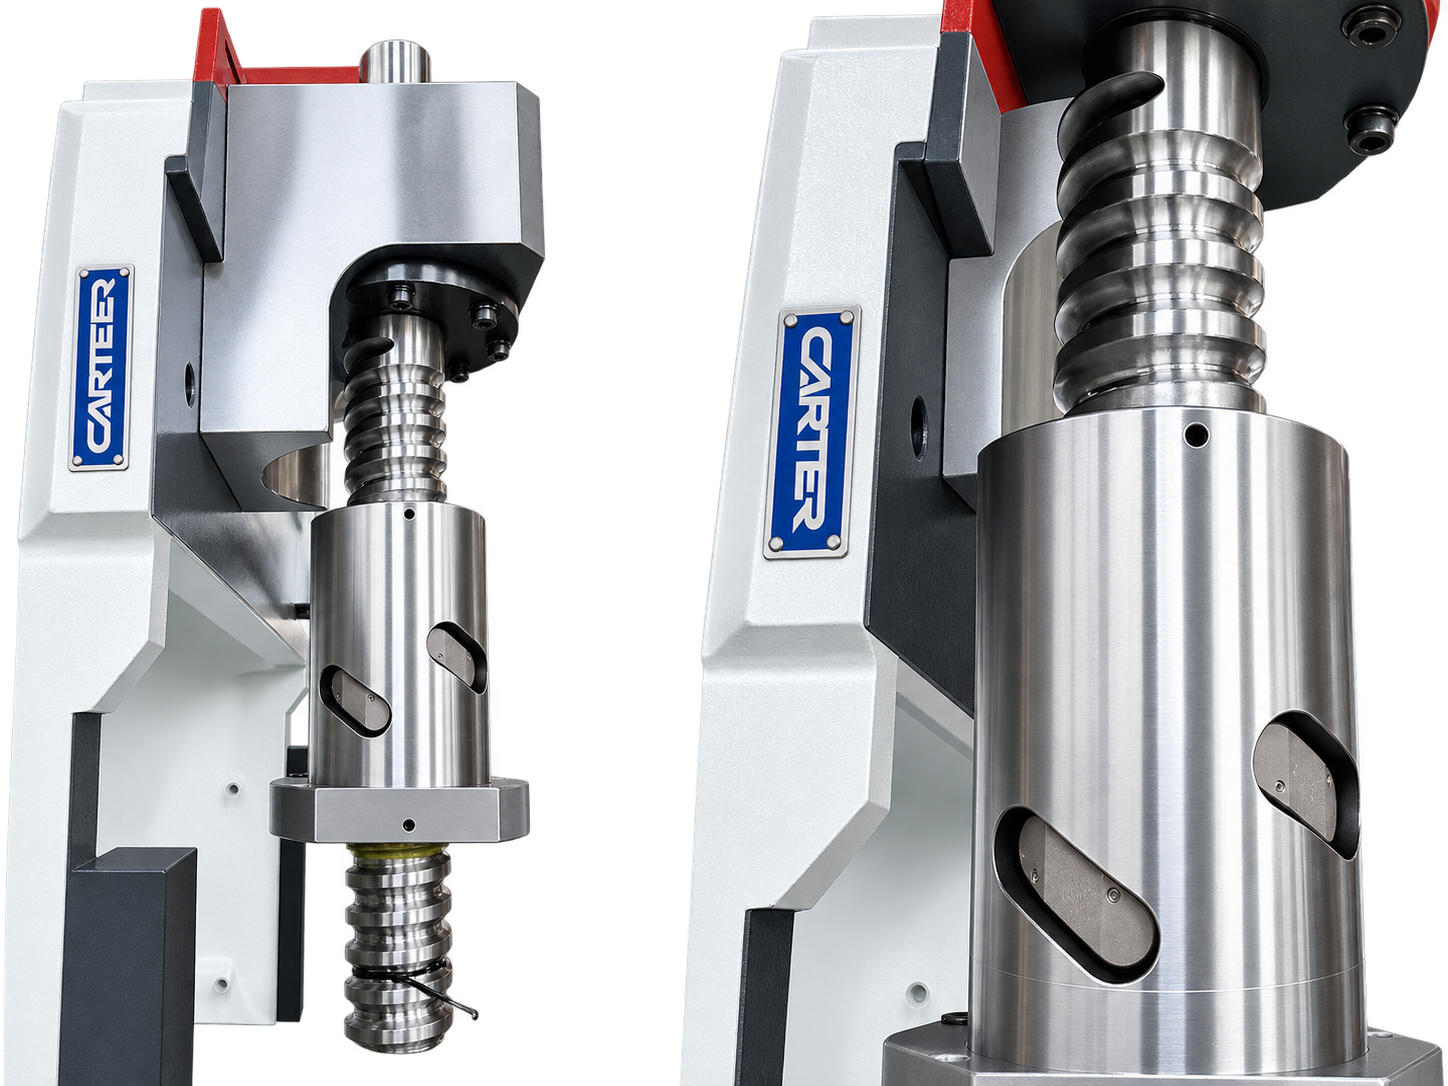
Precision ball screws convert servo motor rotation into accurate linear movement for consistent bending and smooth operation.
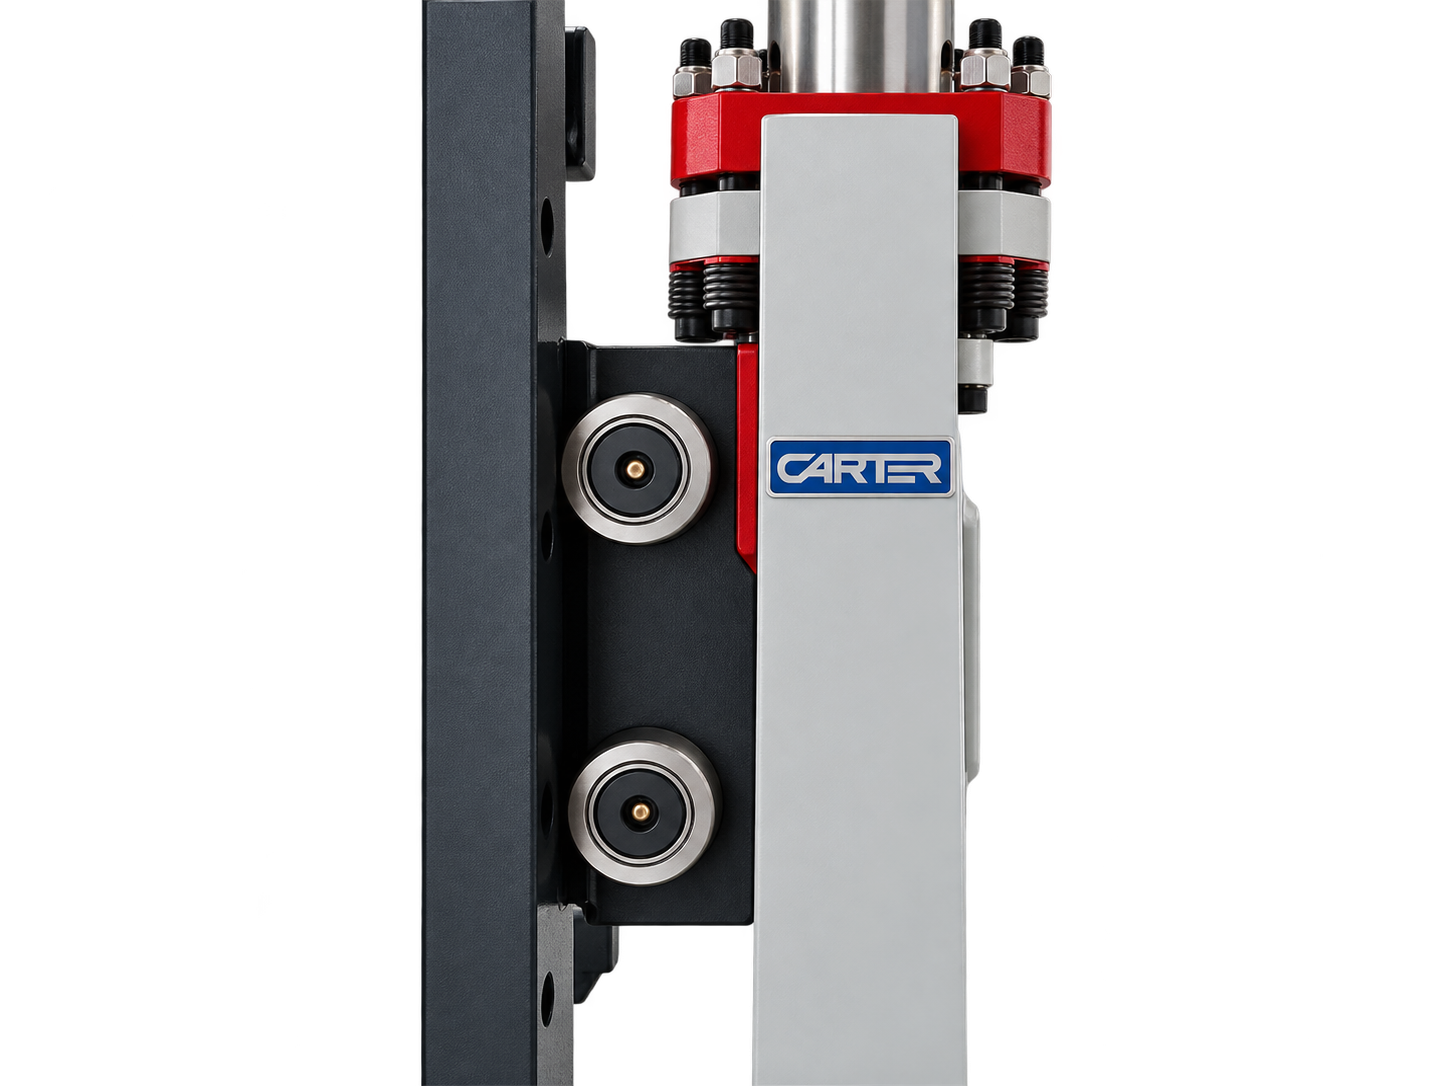
Japanese bearings guide and support the moving assembly, helping maintain balanced travel and repeatable positioning.
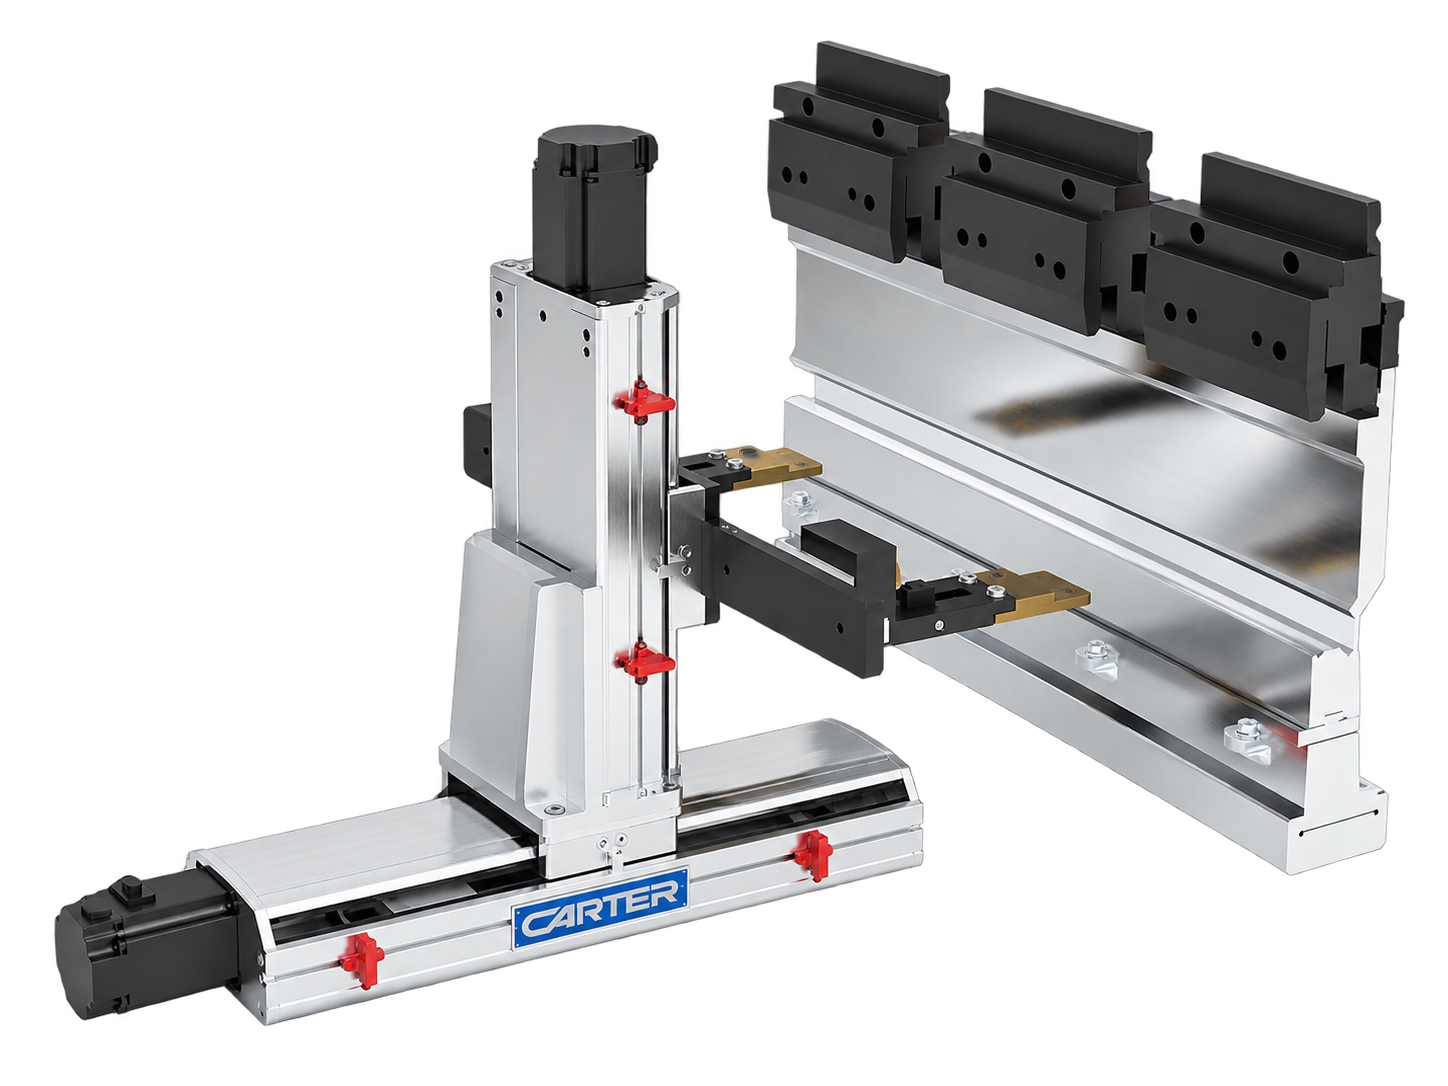
A compact aluminium backgauge combines a rigid structure with servo positioning to support accurate, repeatable component location.
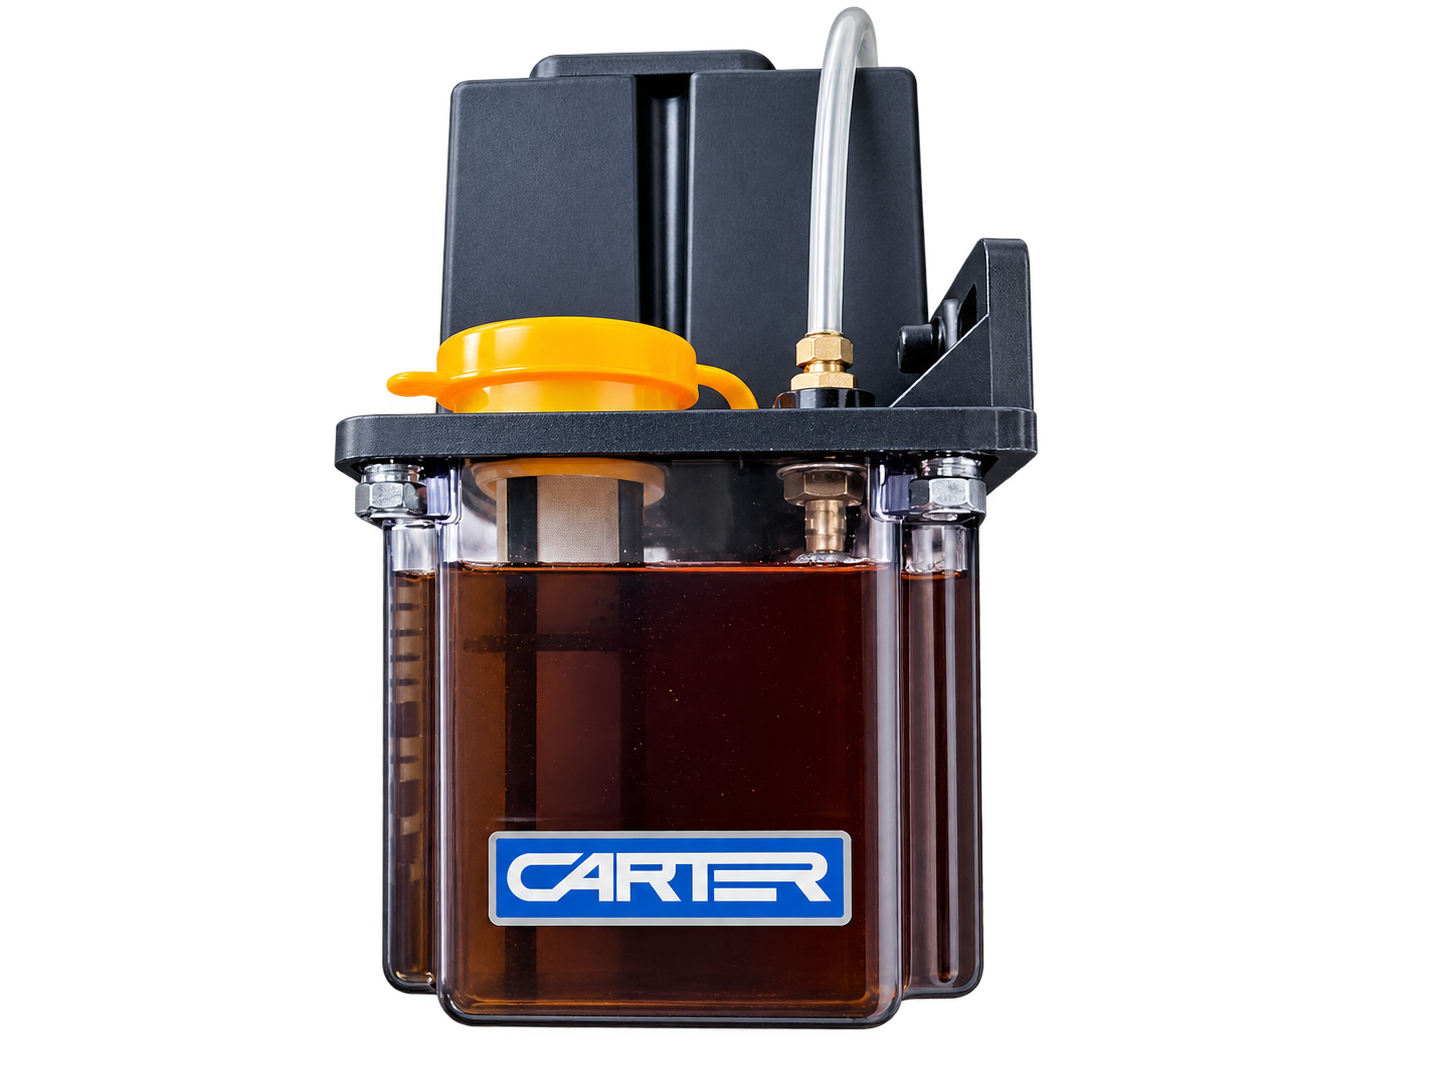
The automatic lubrication system supplies lubricant to the mechanical transmission components to support smooth operation and routine maintenance.
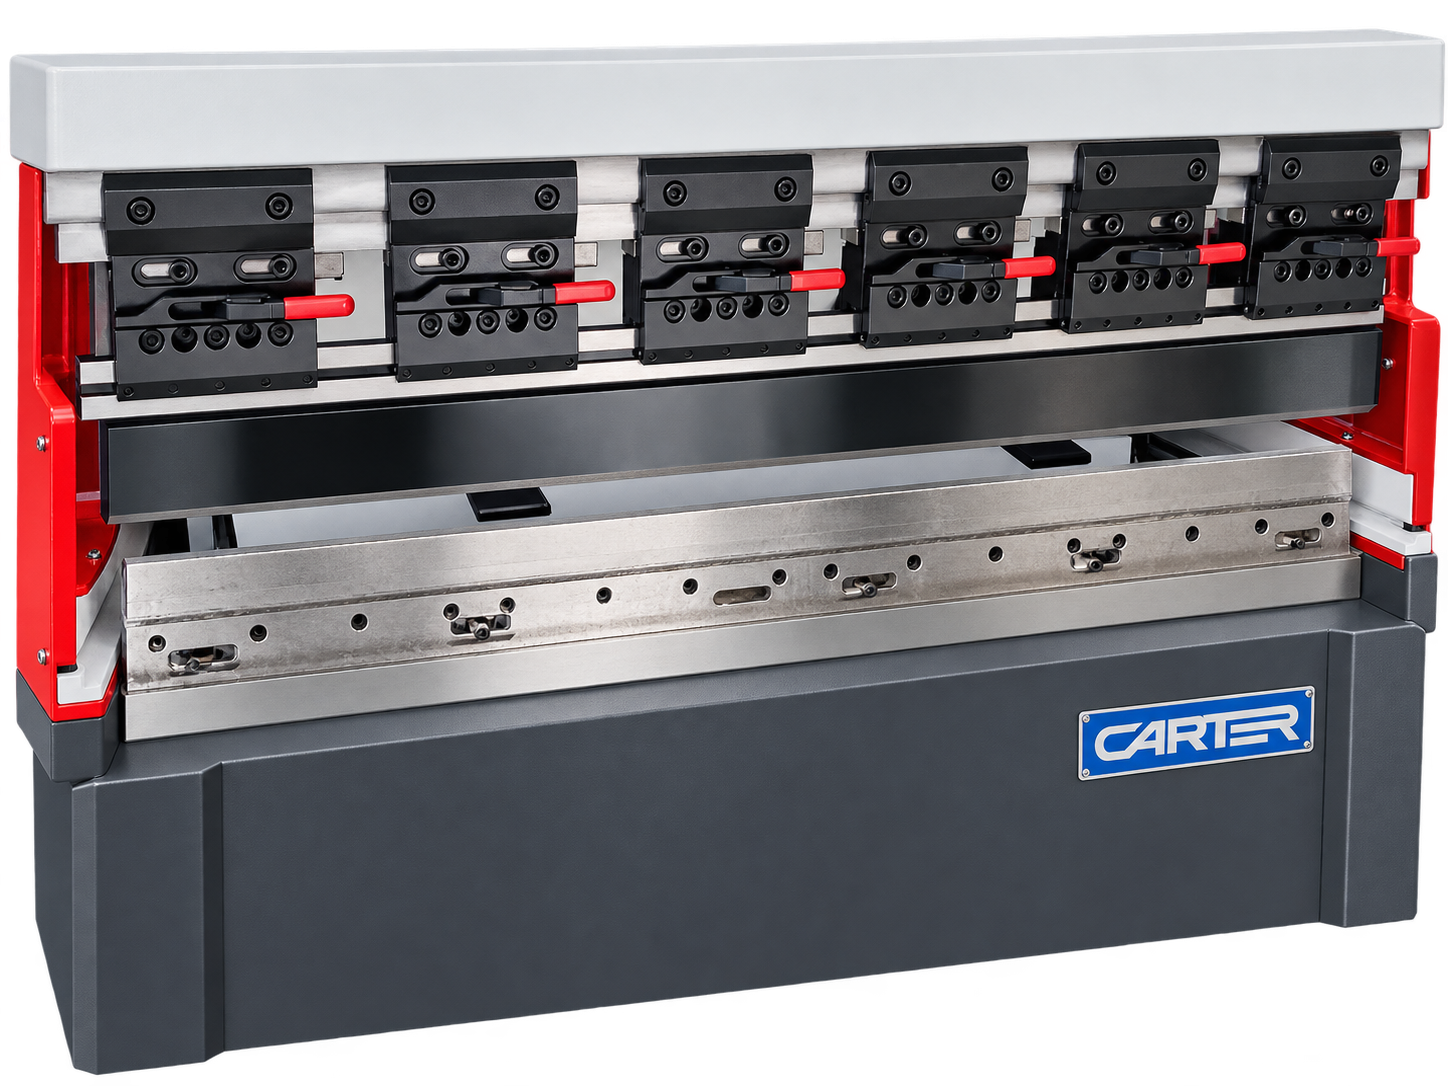
Segmented upper tooling and quick-release clamps make it easier to arrange the tooling around small components and change between jobs.
Final tooling, guarding, electrical supply and machine configuration are confirmed in your quotation.
30% deposit with order. Balance before delivery/collection. Terms and conditions apply.
Prices exclude VAT and delivery. Commissioning and basic training included.
Built around the detail
The all-electric drive removes the need for hydraulic oil, while the compact layout keeps the controls and bending area close to the operator.
Request a quotation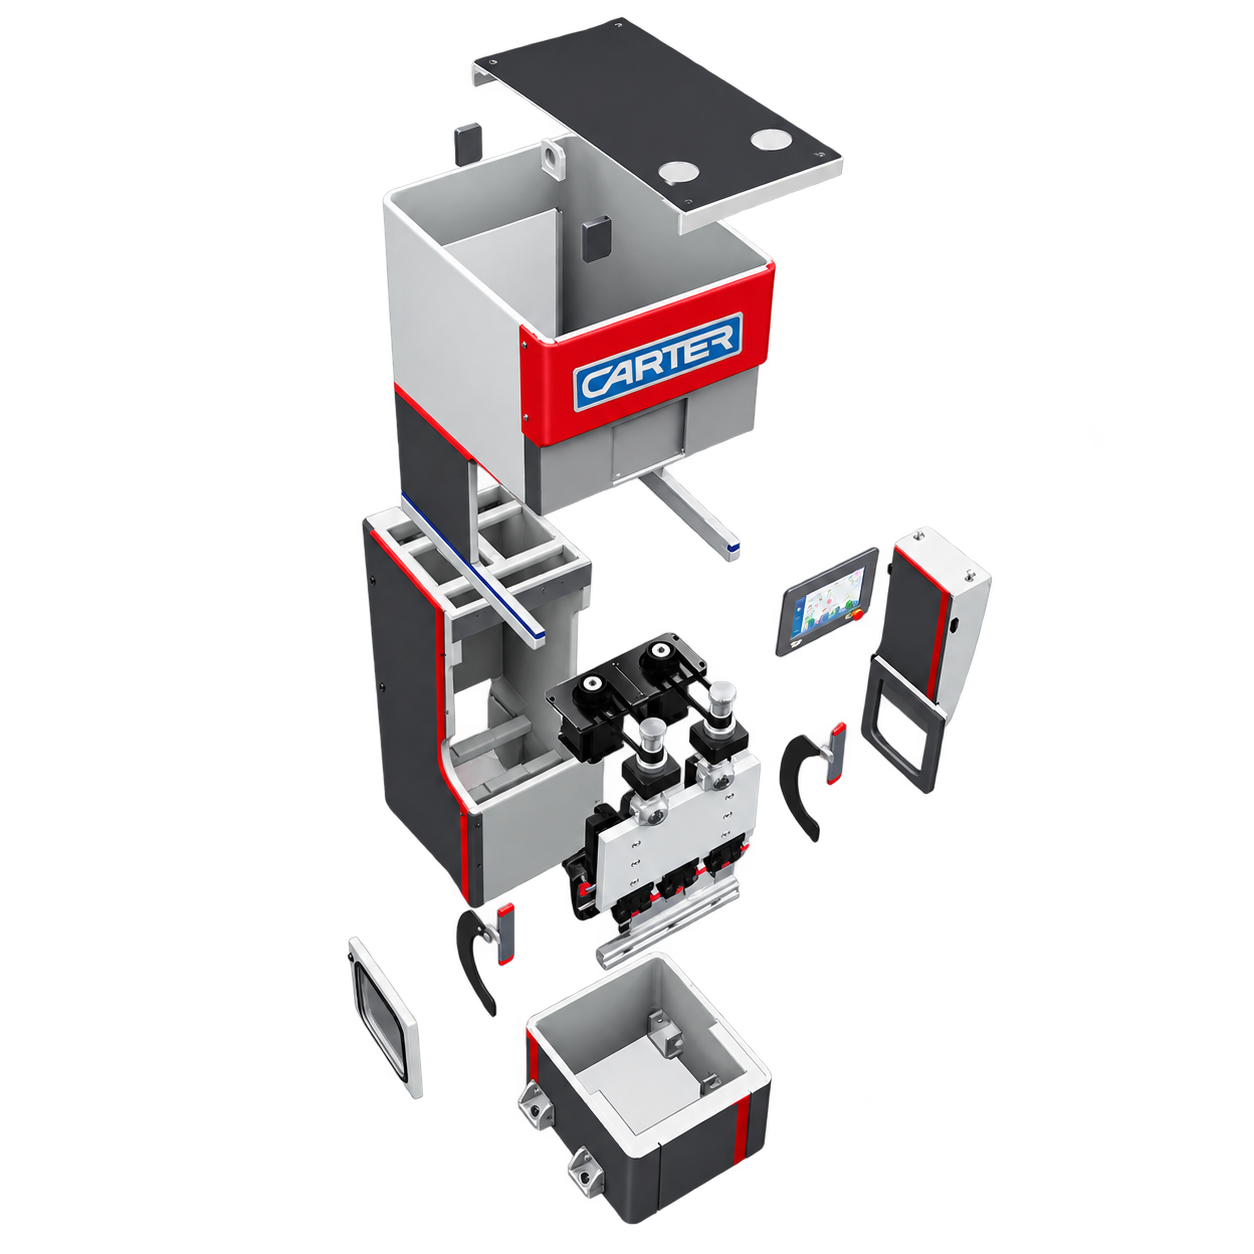
New Carter press brakes include commissioning and basic training.
Telephone and email technical advice continues after the warranty ends. Parts, repairs and engineer visits are chargeable unless covered by warranty.
Delivery, offloading and positioning are quoted for your machine and site. Finance is subject to approval.
Send your material, thickness, bending length and a drawing. We can discuss the machine, tooling and delivery together.
Use the manual for the exact model and fitted equipment. These guides support training and job planning; they do not authorise a setup or replace a site-specific risk assessment.
Workshop video
A 58-second guide to tooling, clearance, bend sequence, hole spacing and first-part inspection.
Watch with sound or follow the on-screen captions. Video in English.
Read the bending guideBehind the build
See the frames and beams for CARTER press brakes during production, from heavy steel structures to machining of the working faces.
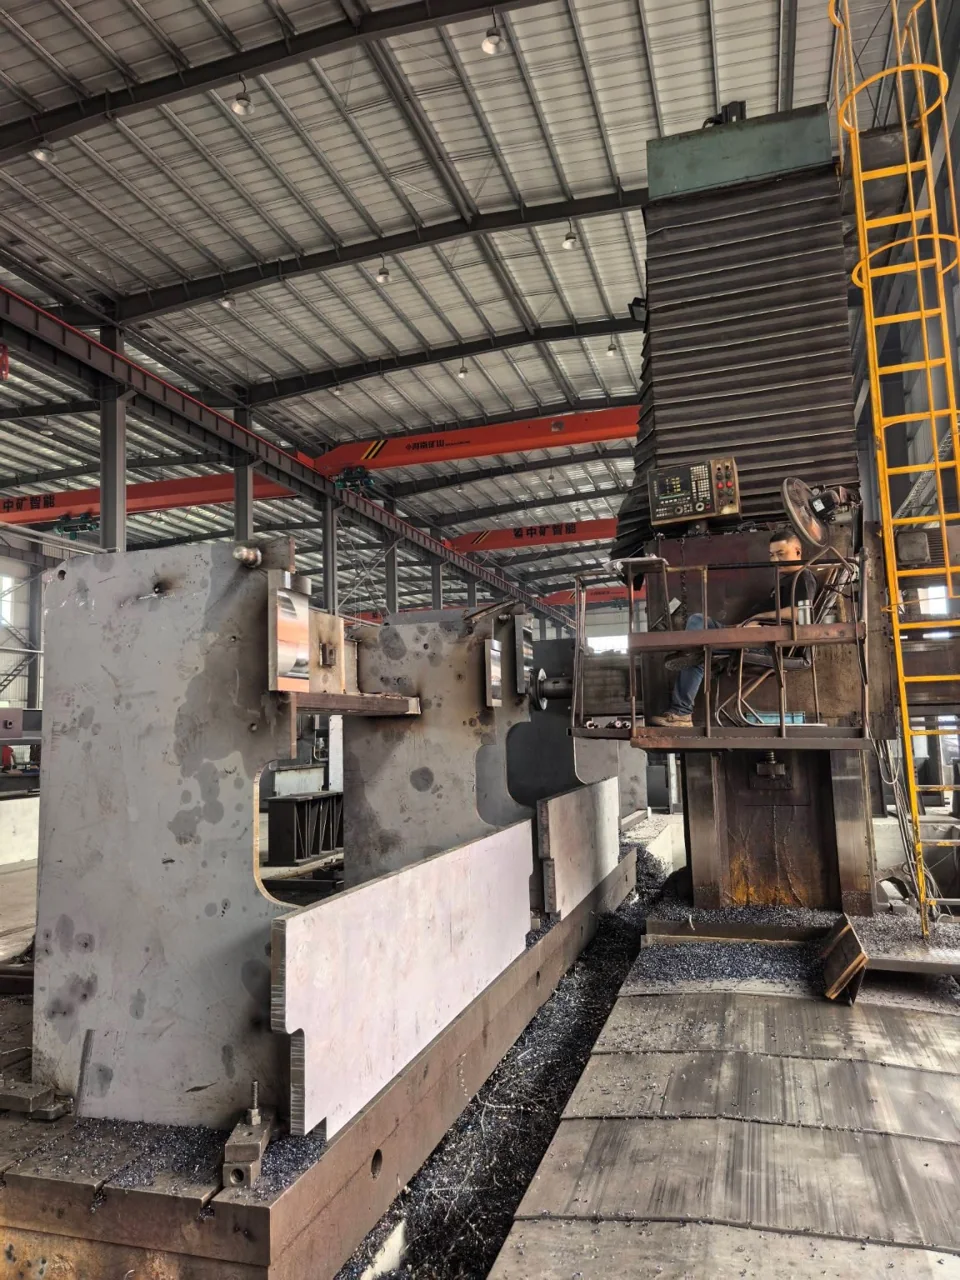
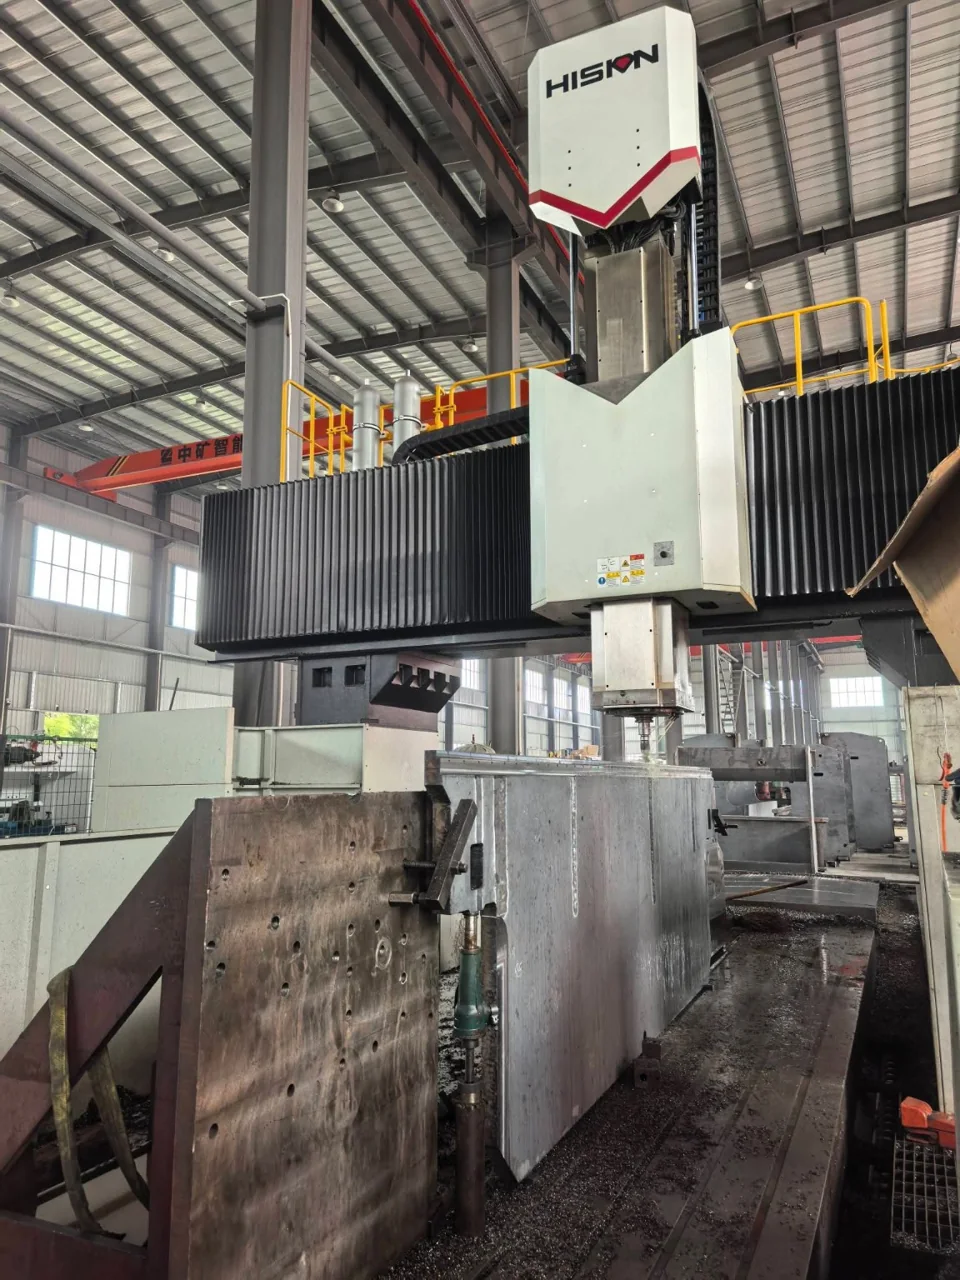
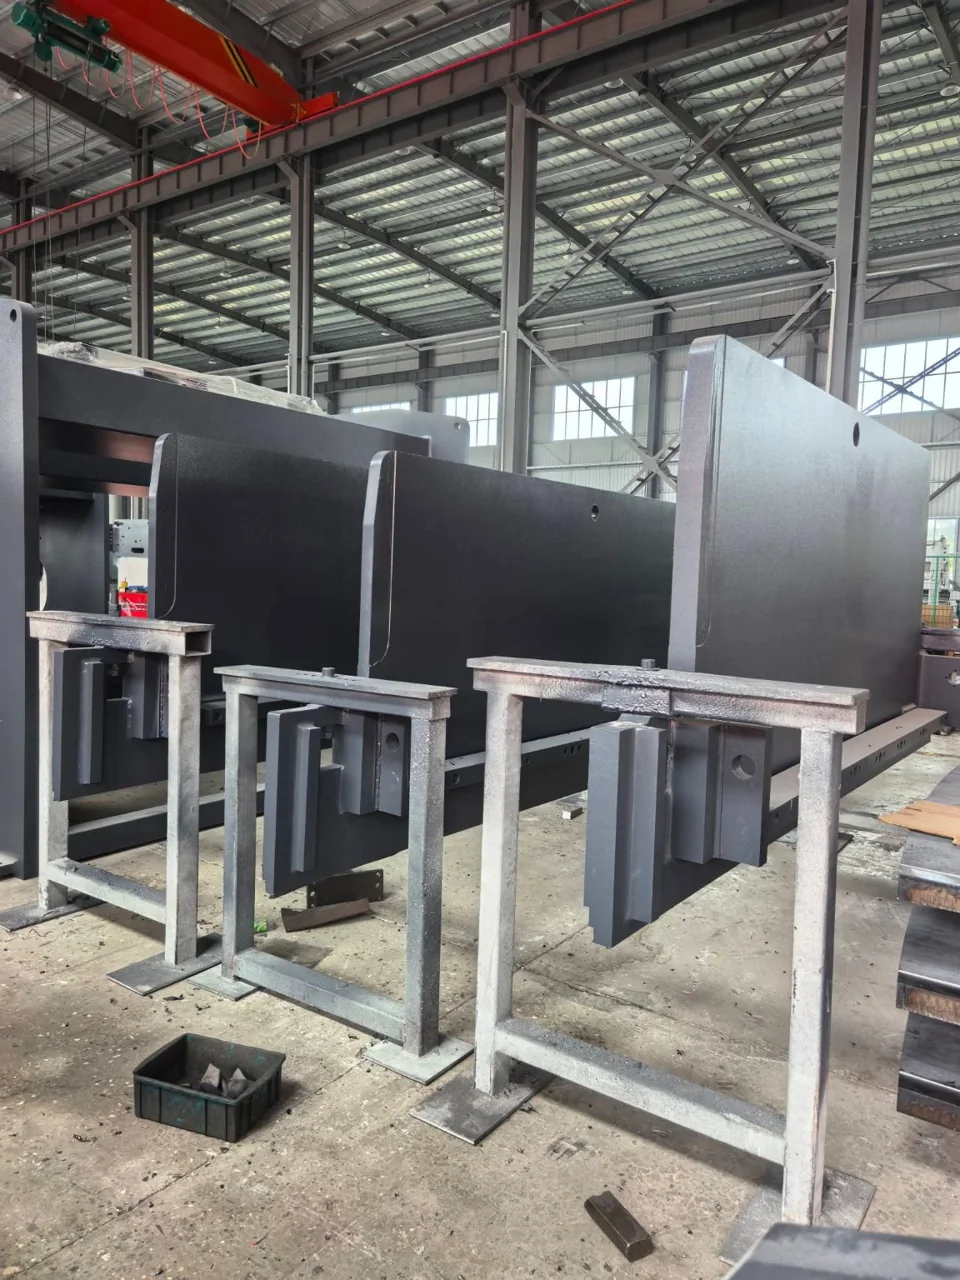
Production photographs from the CARTER press brake range. Frame design and construction vary by model.
Discuss your press brake requirementsCARTER WORKSHOP GUIDE
See how inside radius, K-factor and bend deduction affect the finished part.